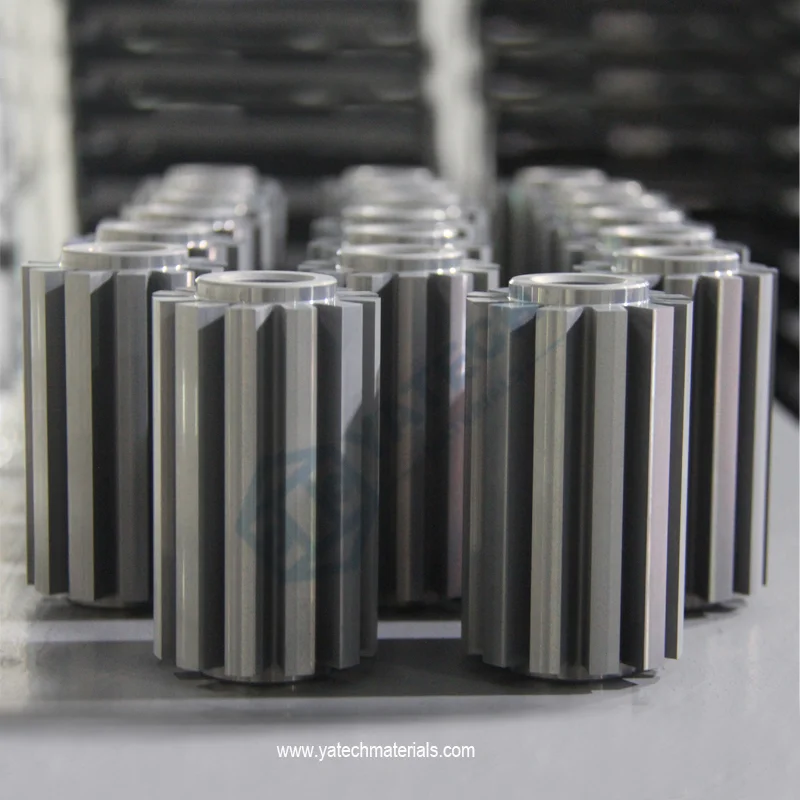
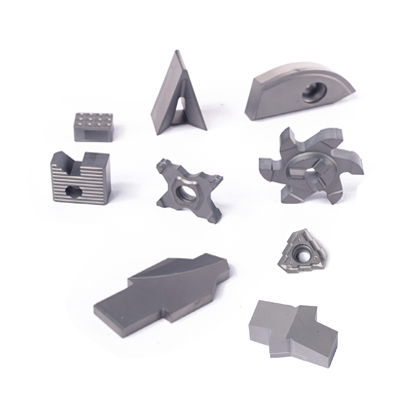
Press-formed carbide near-net blanks for gear hobs, indexable inserts, circular saw discs, полоски, saw tips and slitter knives. Six families, one press house: press tooling for every profile below, 0.3–0.5 mm grinding stock on formed surfaces, and a batch certificate with every lot. If your drawing shows a shape you would otherwise machine out of a solid blank, it belongs here.
Why press a near-net blank
A gear hob, an insert or a saw disc machined from a solid blank spends tungsten carbide turning into chips — the outer shape is already known before the first wheel touches it. Pressing the shape near net removes most of that roughing operation, and it removes it before the expensive part: the finish grind, the coating, the inspection.
What you get is not a finished tool. It is a sintered and HIP-consolidated body with 0.3–0.5 mm of stock on the formed profile, in the grade you specify, with enough dimensional control that your first grinding pass is a finishing pass rather than a shaping pass. Every family below is quoted against your drawing, not against a catalogue number — the catalogue numbers exist so that standard items ship from stock.
The six families
Pick the family your finished tool comes from. Each card carries the size envelope and the Марки that normally run on it — the table below is the same six families in one view.
Size and grade reference
| Family | Size range | Typical Марки | Form |
|---|---|---|---|
| Заготовки зуборезного инструмента | OD 25.8–80.8 · ID 9.6–31.6 · L 20–180 mm; shank type DI 16–85 · L 180–330 mm | YU092 · YU25UF · YU20 · YR12ST · YR70 | Near-net preform |
| Заготовки вставок режущего инструмента | ISO shapes: CNMG · DNMG · SNMG · TNMG · VNMG | YK05 · YK10H · YK30H · YU20F · YM15 | Pressed and ground |
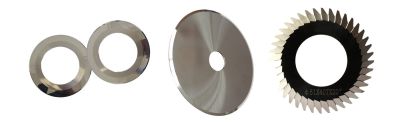
| Circular Saw Disc Blanks | OD 10–300 · ID 4–120 · T 0.3–20 mm | YU20 · YU20H · YU20F · YU25U · YU15 | Ground blank |
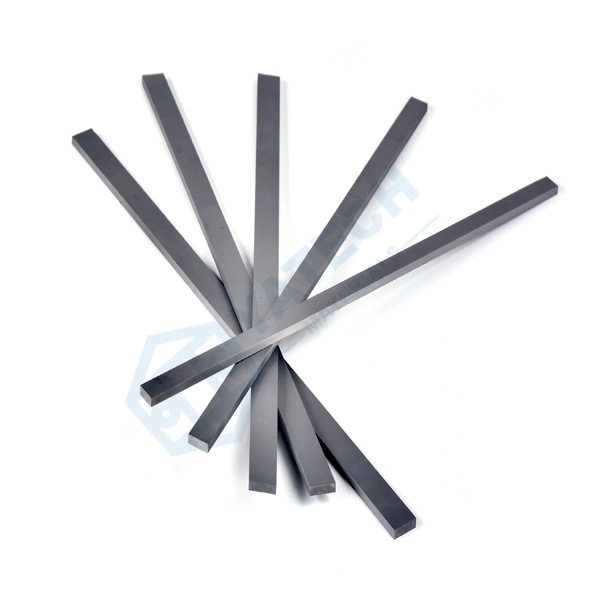
| Твердосплавные полоски | T 2–15 · W 3–30 · L 330 mm, max 2600 mm | YK30 · YK10 · YK05 · YU20 · YU10 | Blank or top/bottom ground |
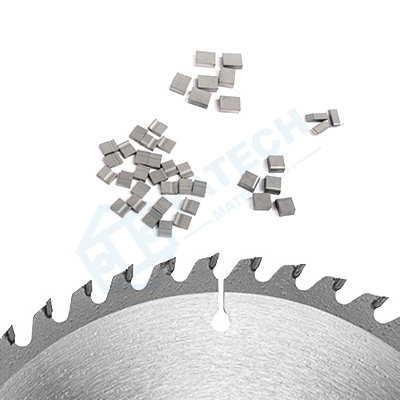
| Твердосплавные зубчатые напайки для пил | Standard sizes from stock · custom to drawing | YM01 · YM03 · YM35 · YF5 | Finished, ready to braze |
| Лезвие для резки карбида вольфрама | OD 20–340 · ID 3–280 · T 1.6–30 mm; OD ±0.2 | YA25UF · YA30K · YA05U · YA10U · YA30U | Ground, finished |
Sizes shown are the standard production envelope for each family. Outside it, ask — an unusual size is usually still possible, it just stops being a stock item.
Note on the last two families. Saw tips and slitter blades are supplied finished rather than as blanks — you braze or mount them, you do not grind them. They sit in this group because they are bought by the same tool-making shops, on the same order, against the same grade logic. If you are looking for a body to grind yourself, you want the saw disc or the полоска above.
How to choose: work backwards from the finished tool
The blank follows from the tool, not the other way round. Three questions settle most enquiries:
| What the finished tool is | The blank you want |
|---|---|
| A hob, a skiving cutter or a stick blade — toothed form, high length-to-diameter | Gear cutting tool blank, preformed to the tooth blank envelope |
| An indexable insert — small, high volume, tight top-face tolerance | Insert blank, pressed to ISO class and ground on the seating faces |
| A saw body or slitting disc — thin, large diameter, needs flatness | Circular saw disc blank, ground, checked for flatness before tooth cutting |
| A knife, forming tool or wear полоска — long rectangular section | Карбид полоска, blank or ground top and bottom |
| A brazed tooth — the tip is the cutting edge, the body is steel | Saw tip, finished and ready to braze |
| A slitting knife — thin disc with a ground cutting edge | Slitter blade, finished to OD/ID/thickness tolerance |
If two rows both look plausible, the deciding factor is usually who does the grinding. A shop that grinds in house buys a blank with 0.3–0.5 mm of stock and a known grade. A shop that does not buys the finished part. Do not order a blank because it is cheaper per piece if you have no way to hold the finished tolerance afterwards.
Grades: the second half of the specification
A blank is only half specified by its shape. The other half is the grade, and for tool blanks the grade argument is usually about edge retention against impact, not hardness alone.
- Ю серия — the gear cutting and insert workhorse. Ultra-fine to sub-micron, 0.2–0.8 µm grain, 6–12% Co, HRA 91.7–93.9. YU092 sits at the hard end for fine modules and finishing passes; YU20 at the tough end for interrupted cuts.
- YR series — YR12ST and YR70, added to the 2026 catalogue. Sub-micron 0.7–0.8 µm, 12% Co, HRA 91.3–91.6 and a typical transverse rupture strength of 4000 MPa: the two Марки to pick when the tooth is long and the machine is not rigid.
- YK series — inserts and полоски. Fine to medium grain, 1.0–2.3 µm, 6–8% Co, HRA 90.1–92.0. YK05 for particle board and finishing work, YK30 for solid wood and heavy sections.
- YM, YF, YG and YW series — saw tips. 2.8–11% binder, HRA 87.0–94.8, matched to the ISO code the tip sits in rather than to a single hardness target.
- серия Я — slitter blades. Sub-fine to super-fine, 6–15% Co, HRA 88.5–93.2, chosen by whether the workpiece is corrugated board, composite or non-ferrous.
Two Марки can carry the same name and differ by 2 HRA and 500 N/mm² depending on whether they were vacuum or HIP sintered. That is why every lot ships with its own certificate rather than a catalogue page: density by Archimedes, hardness HRA, coercivity HС, magnetic saturation, porosity to ISO 4505, grain size to ASTM E112.
What a quotation needs
Six lines is enough to quote. An incomplete enquiry is still worth sending — if the family and the job are clear, we fill in the rest and mark our assumptions on the quote rather than waiting for a reply.
| Line | Example |
|---|---|
| Family | gear cutting tool blank / insert blank / saw disc / полоска / saw tip / slitter blade |
| Dimension | OD 32.8 × ID 12.6 × L 60 mm, or 2 × 12 × 330 mm полоска |
| Grade or job | YK10H, or “1.2379 at 58 HRC” if you would rather we choose |
| Quantity | 10 pcs sample, then 500 pcs / quarter |
| Drawing | PDF or DXF if the profile is not in the standard range |
| Delivery | FOB Shanghai / CIF / DDP + required date |
Indicative lead times: stock sizes 5–10 working days; non-stock in an existing grade 12–20 working days; a new die or a new grade 20–30 working days, counted after drawing approval and die sign-off. Sampling runs 7–15 working days, 6–20 pieces from production tooling, quoted separately from the production order.
Часто задаваемые вопросы
What is the difference between a carbide blank and a finished carbide part?
A blank is sintered close to the final shape but left oversize — typically 0.3–0.5 mm of stock on the formed profile — so that you can grind it to your own tolerance, edge geometry and coating. A finished part is delivered at final dimension and is ready to use or to braze. Blanks are cheaper per piece but assume you have grinding capacity and a way to inspect the result.
How much grinding stock should I allow on a preform?
Our standard is 0.3–0.5 mm on the formed profile. Go to the lower end when your grinder holds tight tolerances and the profile is simple; stay at 0.5 mm when the drawing has thin sections, deep pockets or a heat treatment step between pressing and finish grinding. If you tell us the stock you want, we press to it rather than defaulting.
Can you press a shape that is not in the catalogue?
Yes — that is what the preform family exists for. Send a PDF or DXF. A new die carries a tooling cost and a 20–30 working day lead time from drawing approval, and the die is held for your account so repeat orders do not pay for it again. Grooved, tapered and T-section profiles to 400 mm long are all within range.
Which grade should I choose for a gear cutting blank?
Start with YU20 — sub-micron, 10% Co, HRA 91.8 — for general hobbing and power skiving. Where the module is fine and the failure mode is flank wear, step up to YU092 (0.2–0.4 µm, HRA 93.3) or YU25UF (0.4–0.5 µm, HRA 92.5). Where the gash is interrupted or the machine lacks rigidity, YR12ST and YR70 (both 12% Co, 0.7–0.8 µm, HRA 91.3–91.6, 4000 MPa TRS) trade a little hardness for edge strength. Send the workpiece hardness and the module and we will name one grade rather than a range.
What is the minimum order and can I test before committing?
Standard stock sizes start at 10 pieces. Samples run 6–20 pieces from production tooling in 7–15 working days, so what you test comes off the same die as the production order rather than a laboratory billet. Sampling is quoted separately. For a new preform, die sign-off happens before sampling, not after.
Do blanks ship with a material certificate?
Yes. Each lot carries a certificate of typical values recording density, hardness HRA, coercivity in kA/m, magnetic saturation as a percentage of pure cobalt, porosity to ISO 4505 and grain size to ASTM E112. Mill certificate and third-party inspection are available on request. Ask for a specimen certificate with the quotation if your incoming inspection needs to see the format before a first order.