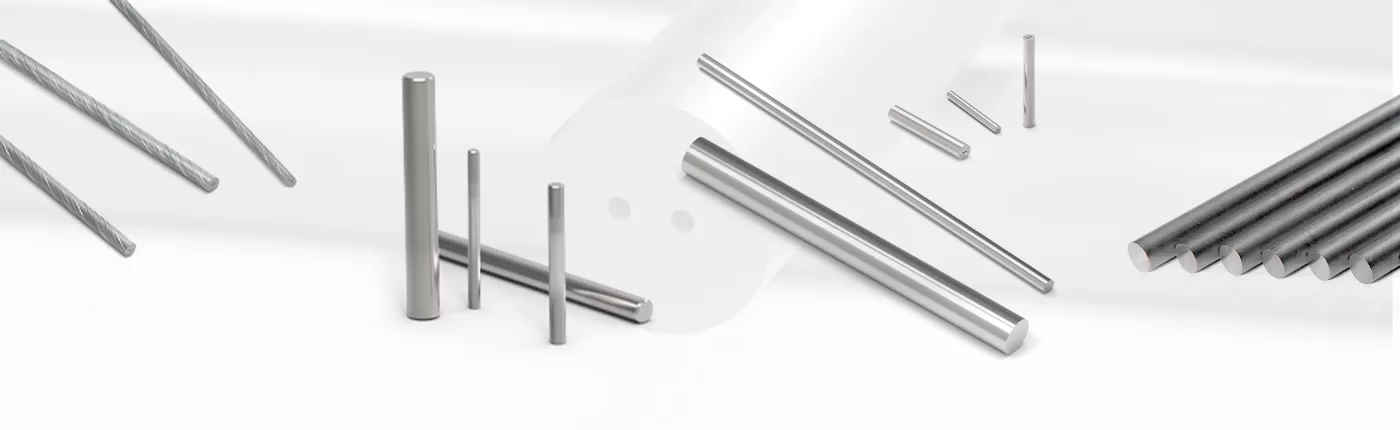
Solid tungsten carbide rods are the blank most round tools start from: no bore, no helix, just WC-Co pressed, sintered, HIPed and centreless-ground to a class your collet can actually hold. We supply them from Ø1.0 to Ø42.0 mm in 310 or 330 mm, either as an as-sintered blank with +0.30 mm on diameter or ground h5, h6 or h7, chamfered or left square for brazing. Because the section is full, a solid rod carries the highest bending load of any pattern we press — which is why it stays the default for end mills, reamers, boring bars and any tool where grinding removes more than half the diameter.
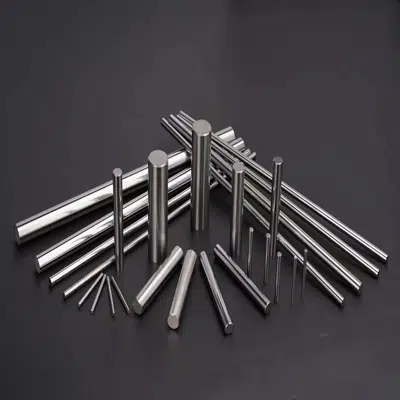
What “solid” changes about the blank
A coolant-hole rod gives up 5–8 % of its section to the bore and the web around it. That is a fair trade when the tool needs coolant delivered at the cutting edge; it is a pure loss when the tool runs under external coolant or needs every newton of bending strength it can get. Solid rod keeps the full circle, so the same outside diameter is stiffer, straighter after grinding and cheaper per millimetre.
The limit is reach. Past about 3×D in a drilled hole, chip evacuation becomes the failure mode rather than strength, and a bore starts to pay for itself. If that is where your tool sits, read the straight coolant rod page instead — the pattern has to be decided before the rod is pressed, not after it is ground.
Four ways to buy the same rod
The material is identical in all four. What changes is how much grinding you have already paid for, and how much stock you want to keep for your own finish pass.
| Option | What you receive | Ø tolerance | Surface Ra | Where it fits |
|---|---|---|---|---|
| 01 · As-sintered blank | Pressed and sintered, +0.30 mm on diameter, cut to length | +0.30 | 3.2 µm | You grind the OD in one pass and want the lowest cost per piece |
| 02 · Ground h6 | Centreless ground, diameter and roundness set in one pass | h6 | 0.2–0.4 µm | Standard tools, clamped in a collet or a ground bore |
| 03 · Chamfered | Ground h6 plus 0.5×45° or 1.0×45° chamfer on both ends | h6 | 0.2–0.4 µm | The default when the rod goes straight into a collet and you want no burr at the end face |
| 04 · Welded chamfer | Ground h6 with a blunt land instead of a ground chamfer | h6 | 0.2–0.4 µm | Brazing into a steel shank: the land holds the braze instead of shedding it |
h5 is a finishing pass on top of h6 and adds 3–5 working days. Ask for it when the collet bore is tighter than 0.008 mm — below that, h6 will show up as runout and h5 is the only way to hold it. Above it, h5 buys nothing you can measure.
Tolerances, ground against blank
Two columns, because the decision is usually made on a drawing rather than a catalogue page. The blank column is what the press and the sintering furnace deliver; the ground column is what the centreless grinder adds.
| Feature | Ground (h5 / h6 / h7) | As-sintered blank |
|---|---|---|
| Diameter | Per ISO 286, upper deviation 0 | +0.30 mm |
| Roundness | ≤ ½ of the diameter tolerance | Not specified |
| Straightness | 0.05 mm per 100 mm | 0.30 mm per 100 mm |
| Length | ±0.30 mm | ±0.50 mm |
| End face squareness | 0.05 mm | 0.15 mm |
| Surface roughness | Ra 0.2–0.4 µm | Ra 3.2 µm |
Straightness is the number that decides how a flute grind behaves. Grind a rod that bows by 0.3 mm and the flutes come out deeper on one side along its length; the tool then cuts oversize exactly where the load is highest. 0.05 mm per 100 is held on every ground rod, not sampled.
Metric sizes, Ø1.0–12.0 mm
Ground h6, standard length 330 mm, chamfered both ends. Weight is calculated at 14.45 g/cm³; other grades differ by up to 6 %.
| Ø (mm) | h6 tolerance | Chamfer | kg/m | Order code |
|---|---|---|---|---|
| 1.0 | 0 / −0.006 | 0.5×45° | 0.011 | YSR-0100-330 |
| 1.2 | 0 / −0.006 | 0.5×45° | 0.016 | YSR-0120-330 |
| 1.5 | 0 / −0.006 | 0.5×45° | 0.026 | YSR-0150-330 |
| 1.8 | 0 / −0.006 | 0.5×45° | 0.037 | YSR-0180-330 |
| 2.0 | 0 / −0.006 | 0.5×45° | 0.045 | YSR-0200-330 |
| 2.5 | 0 / −0.006 | 0.5×45° | 0.071 | YSR-0250-330 |
| 3.0 | 0 / −0.006 | 0.5×45° | 0.102 | YSR-0300-330 |
| 3.175 | 0 / −0.008 | 0.5×45° | 0.114 | YSR-0318-330 |
| 3.5 | 0 / −0.008 | 0.5×45° | 0.139 | YSR-0350-330 |
| 4.0 | 0 / −0.008 | 0.5×45° | 0.182 | YSR-0400-330 |
| 4.5 | 0 / −0.008 | 0.5×45° | 0.230 | YSR-0450-330 |
| 5.0 | 0 / −0.008 | 0.5×45° | 0.284 | YSR-0500-330 |
| 5.5 | 0 / −0.008 | 0.5×45° | 0.343 | YSR-0550-330 |
| 6.0 | 0 / −0.008 | 0.5×45° | 0.409 | YSR-0600-330 |
| 6.5 | 0 / −0.009 | 0.5×45° | 0.479 | YSR-0650-330 |
| 7.0 | 0 / −0.009 | 0.5×45° | 0.556 | YSR-0700-330 |
| 8.0 | 0 / −0.009 | 0.5×45° | 0.726 | YSR-0800-330 |
| 9.0 | 0 / −0.009 | 0.5×45° | 0.919 | YSR-0900-330 |
| 10.0 | 0 / −0.009 | 0.5×45° | 1.135 | YSR-1000-330 |
| 11.0 | 0 / −0.011 | 1.0×45° | 1.373 | YSR-1100-330 |
| 12.0 | 0 / −0.011 | 1.0×45° | 1.634 | YSR-1200-330 |
Also available in 310 mm, in h5 or h7, and unchamfered. Add the tolerance and end letter to the code: YSR-0800-330-H6-C is the full form.
Metric sizes, Ø13–32 mm, and inch
Large rod is ground on the same line as small rod — centreless, one pass, diameter and roundness established together. The only difference is that a billet above Ø32 is pressed singly rather than in a multi-cavity die.
| Ø (mm) | h6 tolerance | kg/m | Order code |
|---|---|---|---|
| 13 | 0 / −0.011 | 1.92 | YSR-1300-330 |
| 14 | 0 / −0.011 | 2.22 | YSR-1400-330 |
| 16 | 0 / −0.011 | 2.90 | YSR-1600-330 |
| 18 | 0 / −0.011 | 3.68 | YSR-1800-330 |
| 20 | 0 / −0.011 | 4.54 | YSR-2000-330 |
| 22 | 0 / −0.011 | 5.49 | YSR-2200-330 |
| 25 | 0 / −0.013 | 7.09 | YSR-2500-330 |
| 28 | 0 / −0.013 | 8.90 | YSR-2800-330 |
| 30 | 0 / −0.013 | 10.21 | YSR-3000-330 |
| 32 | 0 / −0.016 | 11.62 | YSR-3200-330 |
Inch sizes are ground from metric billets to the equivalent diameter, and 12″ or 13″ lengths are available on request.
| Inch | mm | h6 tolerance | kg/m |
|---|---|---|---|
| 1/8″ | 3.17 | 0 / −0.008 | 0.11 |
| 3/16″ | 4.76 | 0 / −0.008 | 0.26 |
| 1/4″ | 6.35 | 0 / −0.009 | 0.46 |
| 5/16″ | 7.94 | 0 / −0.009 | 0.71 |
| 3/8″ | 9.52 | 0 / −0.009 | 1.03 |
| 1/2″ | 12.70 | 0 / −0.011 | 1.83 |
| 5/8″ | 15.88 | 0 / −0.011 | 2.86 |
| 3/4″ | 19.05 | 0 / −0.013 | 4.12 |
| 7/8″ | 22.22 | 0 / −0.013 | 5.61 |
| 1″ | 25.40 | 0 / −0.013 | 7.32 |
| 1-1/4″ | 31.75 | 0 / −0.016 | 11.44 |
| 1-1/2″ | 38.10 | 0 / −0.016 | 16.47 |
Stock, lengths and what is pressed to order
Six diameters are held in inventory in two grades — h6 ground, 330 mm, chamfered: Ø3.0, 4.0, 6.0, 8.0, 10.0 and 12.0 mm in YU25UF and YU092. Between them they cover most of what a jobbing shop grinds in a month, and they ship from stock rather than from a press schedule.
Everything else is pressed to order, typically 10–20 working days. Three ranges step up: above Ø32 the billet is pressed singly, 15–25 days; below Ø3.0 the rod is pressed in a single cavity and ground between centres, which is why the price per piece rises sharply as the diameter falls; and h5 adds a finishing pass plus 3–5 days.
Two lengths are standard. 310 mm suits 40-taper and shrink-fit holders, 330 mm suits everything else. Both are saw-cut and then ground square, so length is a finishing dimension rather than a nominal. Any length from 50 to 330 mm can be cut to order, ground square to ±0.30 mm; below 50 mm the chamfer becomes a deburr only.
Choosing the blank for a finished tool
The rule we use: blank length = flute length + 1.5× the shank diameter + 2 mm of grind allowance. Where two diameters are shown, the larger one is for a tool with an undercut neck.
| Finished tool | Cutting Ø (mm) | Blank Ø (mm) | Blank length (mm) |
|---|---|---|---|
| Micro end mill, 2-flute | 1.0–1.5 | 3.0 | 50 |
| Micro drill, PCB | 0.5–1.0 | 3.175 | 38 |
| End mill, 3-flute, aluminium | 6 | 6.0–6.5 | 57–64 |
| End mill, 4-flute, steel | 10 | 10.0–11.0 | 72–80 |
| End mill, long reach | 12 | 12.0 | 100–120 |
| Corner-radius, necked | 8 | 8.0 | 60 |
Odd diameters are not a problem. Rod is ground from the nearest billet, so Ø7.3 or Ø11.8 is a normal order — send the finished tool dimension and we name the nearest stock size that still leaves grinding stock. A ground h6 blank leaves 0.05–0.10 mm of radial stock for your finish pass; drop a size only to grind out a defect, never to save material.
Grades for solid rods
Solid rod comes in the twelve round-tool grades and the six wear grades. Stock diameters are held in YU25UF and YU092, which between them cover general steel and aluminium work in YU25UF and hardened steel, finishing and sub-micron work in YU092. Grades ending UF are ultra-fine (grain 0.5 µm or below): sharper edge, longer life, less forgiving of an interrupted cut — read the TRS column, not only the hardness.
| Grade | ISO | Co % | Grain (µm) | Density g/cm³ | HRA | TRS N/mm² | K1C MPa·m1/2 | Where it fits |
|---|---|---|---|---|---|---|---|---|
| YU25UF | K20–K40 | 12 | 0.4 | 14.10 | 92.6 | 4 200 | 9.9 | General steel and aluminium, the stock grade for most tool grinding |
| YU20F | K20–K40 | 12 | 0.6 | 14.37 | 92.3 | 4 200 | 10.2 | Same duty as YU25UF with more tolerance of interrupted cuts |
| YU20 | K20–K40 | 10 | 0.8 | 14.40 | 91.9 | 4 000 | 10.5 | Heavier cuts, roughing end mills, tools with a long overhang |
| YU092 | K05–H10 | 9 | 0.2 | 14.44 | 94.0 | 4 100 | 9.1 | Sub-micron grade for finishing, hardened steel above 45 HRC, small diameters |
| YU10UF | K05–K10 | 6 | 0.4 | 14.80 | 94.0 | 3 800 | 9.2 | Wear resistance where the cut is stable and the workpiece abrasive |
| YU15UF | H10–H20 | 8.5 | 0.4 | 14.52 | 93.2 | 4 300 | 9.6 | Hardened steel, high hardness with the toughness to survive a ground edge |
| YMR12T | M20–M40 | 12 | 0.7 | 14.15 | 91.8 | 4 100 | 11.5 | Stainless and duplex, where built-up edge is the failure mode |
| YSR11B | S20–S40 | 11 | 0.8 | 14.15 | 91.5 | 4 100 | 12.1 | Inconel, titanium and heat-resistant alloys |
Typical values for sintered and HIP material, not guaranteed minima. Hardness to ISO 3878, TRS on ISO 3327 B-size test bars, K1C by Palmqvist on polished sections, density by Archimedes. Certified values accompany every batch.
How the order code reads
The code is read left to right, and it is the same grammar across all four families we press — solid rod, coolant hole, preform and flat bar. YSR-1000-330-H6-C is a solid rod, Ø10.00 mm, 330 mm long, ground h6, chamfered both ends.
| Position | Codes | Meaning |
|---|---|---|
| Family | YSR · YCH · YPF · YFB | Solid rod · coolant hole · preform · flat bar |
| Diameter | 1000 | Diameter in 1/100 mm, so 1000 is Ø10.00 |
| Length | 330 | Millimetres, cut to length |
| Tolerance | H5 · H6 · H7 · BL | Ground class, or BL for an as-sintered blank |
| End | C · S · W | Chamfered · square · welded chamfer |
A blank Ø8 for a jobbing shop grinding its own OD is quoted as YSR-0800-330-BL-S, and the same rod chamfered and ground as YSR-0800-330-H6-C. Quote either form on the enquiry — if the code is wrong for the job we will say so before the order is released, not after the rod is cut.
From powder to a ground rod
The rod is pressed to near-diameter, consolidated so density does not vary along its length, sintered and then HIPed to close residual porosity. YU092 goes through a −196 °C sub-zero treatment between sintering and grinding as standard; on other grades it is available on request. Grinding is centreless in a single pass, which sets diameter and roundness together — there is no second operation that could introduce a lobing error.
The result is a blank whose only variables are the ones on the drawing. Diameter class, straightness, end squareness and surface finish are all specified in the tolerance table above, and each batch ships with its own density, hardness and TRS figures so the material can be checked against the certificate rather than against a catalogue value.
Frequently Asked Questions
What is a solid tungsten carbide rod?
A rod of cemented tungsten carbide with no bore and no helix, pressed, sintered, HIPed and centreless-ground. We supply it from 1.0 to 42.0 mm in 310 or 330 mm, either as an as-sintered blank with +0.30 mm on diameter or ground to h5, h6 or h7, chamfered or left square for brazing. Because the section is full, it takes the highest bending load of any rod pattern we press.
Should I order an as-sintered blank or a ground rod?
Order the blank if you grind the outside diameter in one pass anyway - it is the cheapest per piece and leaves you the most stock. Order ground h6 if the rod goes straight into a collet or a ground bore and you want the diameter, roundness and finish already set. h5 is a finishing pass on top of h6: ask for it only when the collet bore is tighter than 0.008 mm, because above that it buys nothing you can measure and adds 3-5 working days.
Which tolerance class do I need - h5, h6 or h7?
h6 covers most tool grinding and is what we hold in stock. h5 is for a collet bore under 0.008 mm, where h6 would show up as runout. h7 is for a looser location - brazing into a shank, or a holder that clamps on a sleeve. All three are ground on the same line; the class changes the number of passes, not the material.
What is the largest diameter you can supply?
The standard production envelope is 42 mm. Up to 32 mm the rod is pressed in a multi-cavity die and is a normal stock or short lead-time item; above 32 mm the billet is pressed singly, which puts it at 15-25 working days. Above 42 mm we quote it as a custom pressing rather than a rod.
Do you supply inch sizes and longer lengths?
Yes. Inch sizes from 1/8" to 1-1/2" are ground from metric billets to the equivalent diameter, so the tolerance class is the same as the metric table. Standard length is 330 mm, with 310 mm for 40-taper and shrink-fit holders, and 12" or 13" lengths are available on request.
Can I get a length other than 330 mm?
Any length from 50 to 330 mm, saw-cut and then ground square to plus or minus 0.30 mm. Both standard lengths are ground square as well, so length is a finishing dimension rather than a nominal. Below 50 mm the chamfer becomes a deburr only, because there is not enough length left to hold the rod for grinding.
Which grades are held in stock?
Six diameters - 3.0, 4.0, 6.0, 8.0, 10.0 and 12.0 mm - are held as ground h6, 330 mm, chamfered, in YU25UF and YU092. Between them those two grades cover general steel and aluminium work and the harder, finer end of the range. Every other diameter, grade or tolerance is pressed to order, typically 10-20 working days.
How does solid rod differ from coolant-hole rod?
A coolant-hole rod gives up 5-8 % of its section to the bore and the web around it, and gains coolant delivered at the cutting edge. Solid rod keeps the full circle, so the same diameter is stiffer, straighter after grinding and cheaper per millimetre. The practical split is reach: past about 3xD in a drilled hole, chip evacuation becomes the failure mode and a bore starts to pay for itself.
Get a Quote for Solid Tungsten Carbide Rods
Related tungsten carbide products
Solid rod is one blank in a wider rod range. The rest of the family:
- Carbide Rods — the full range, with the tolerance and grade overview for both solid and coolant-hole rod
- Straight Coolant Rods — one or two axial bores for gun drills, reamers and form tools
- Helical Coolant Hole Rods — 30° and 40° helix, 2 and 3 holes, for twist drills and end mills
- Tungsten Carbide Grades — full grade data, ISO classes and the selection matrix
- Carbide Tool Blanks — preforms pressed to drawing for gear cutters, inserts and specials